
Current location: ENGLISh > NEWS > Industry Trends >
Briefly introduce the product characteristics and maintenance methods of gear pu
time:2018-11-15 04:20:08 author:特种泵阀 click:470
Gear pumps need to operate smoothly, with a gear meshing overlap greater than 1. Therefore, there are always two pairs of gears meshing simultaneously, and a portion of the oil is trapped between the enclosed chambers formed by the two pairs of gear teeth. This closed chamber gradually decreases with the rotation of the gear, and then gradually increases again. The reduction in the volume of the enclosed chamber will cause the trapped oil to be compressed, resulting in high pressure and extrusion from the gaps, causing the oil to heat up and causing additional loads on the components; The increase in the volume of the enclosed chamber causes local vacuum, which separates the dissolved gases in the oil and produces cavitation. These will generate strong vibrations and noise, which is the phenomenon of trapped oil in gear pumps.
Harm: When the radial unbalance force is large, it can cause the shaft to bend, the tooth tip to come into contact with the housing, and accelerate the wear of the bearing, reducing its service life.
Method for oil entrapment: Usually, unloading slots are opened on both sides of the cover plate, so that when the volume of the closed chamber decreases, it is connected to the oil pressure chamber through the unloading slot on the left, and when the volume increases, it is connected to the oil suction chamber through the unloading slot on the right.
Comparison between gear pump and screw pump: Both belong to positive displacement pumps, so their performance is basically similar - they can stably transport high viscosity substances and both have higher conveying pressure. But the screw pump has a major drawback that determines its unsuitability - the non streamlined surface of the screw pump and the defects in the chamber determine its short service life, while this pump is easy to transport high viscosity media due to the streamline structure of the rotor and the lack of dead points and non-metallic parts in the rotor chamber. The working principle of Roots pump: Cam pump, also known as Roots pump, stainless steel rotor pump, cam pump, universal conveying pump, high concentration slurry pump, etc. The electric motor reduces the speed through a reducer to bring two synchronous and counter rotating rotors to generate suction (vacuum degree) during the rotation process, thereby sucking in the material to be conveyed.
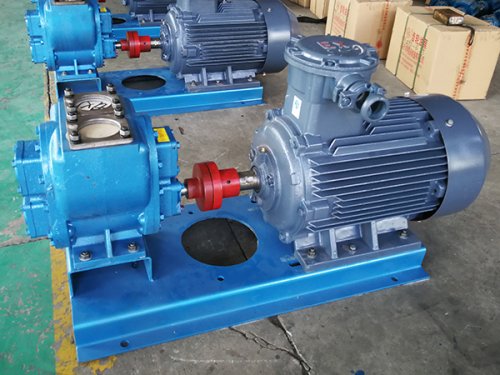
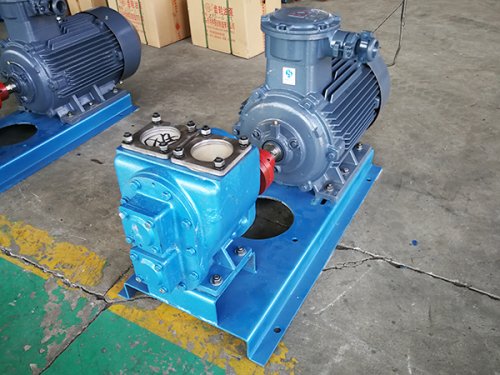
The product features of gear pumps include long service life, maintaining clearance between the two wheels without friction or wear. The contact between rotors ensures long-term use without wear, smooth operation, low noise, and high efficiency. Widely applicable: It is a product that replaces screw pumps for conveying media with high viscosity, concentration, and task containing particles. This pump belongs to the positive displacement pump, and the delivery flow can be easily controlled or made into a variable displacement pump. The output flow rate of a centrifugal pump cannot be controlled and decreases with an increase in drag; This pump has strong self-priming ability, while the centrifugal pump is filled with liquid before starting. The speed of this pump is very low, usually between 200rmp and 600rmp, and the conveyed material is smoothly output without damaging its composition. And the centrifugal pump has a high speed, which is affected by the impact and centrifugal force on the conveyed material.
The maintenance of gear pump components mainly includes the following aspects:
1. Repair of worn gear pump shaft
The wear of the shaft in the gear pump is mainly due to the frictional wear between the two ends of the shaft and the supporting rollers, which reduces the shaft diameter. If there is slight wear, the diameter of the shaft in this area can be increased by plating a layer of hard chromium to make the shaft larger. If the shaft is severely worn, it should be made of 45 steel or 40cr steel again. After rough and fine machining of the shaft blank, the bearing part should be heat treated with a hardness of hrc60-65, and then ground to ensure that the surface roughness ra of the bearing fitting part is not greater than 0.32 μ m; The allowable deviation for roundness and cylindricity of the shaft is 0.005mm; the mating part with the gear should be h7/h6, and the surface roughness ra should not exceed 0.63mm.
2. Repair of gear pump body after wear and tear
The wear on the surface of the pump body is mainly caused by the arc-shaped working surface of the oil suction section. If there is slight wear, you can use an oilstone to remove burrs before use. The pump body is formed by casting cast iron blanks, and new parts should be replaced when severe wear occurs. If the two end faces of the gear inside the pump are ground, the width dimension of the pump body should also be changed to be equal to the size removed by grinding the two ends of the gear. The reprocessed two end faces of the pump body should meet the technical requirements.
3. Repair of worn-out covers on both ends of the gear pump
The end cover of the gear pump is made of cast iron. If there is wear, it can be lightly ground and leveled on a flat plate. If the wear is severe, it should be ground and leveled on a surface grinder. The flat contact between the end cap and the pump body after grinding should not be less than 85% The tolerance for flatness, perpendicularity of the end face to the centerline of the hole, parallelism of the two end faces, and parallelism of the centerline of the two axis holes are all o.olmm. The surface roughness ra after grinding should not exceed 1.5 μ m.
4. Repair and replacement of needle roller bearings for gear pumps
After repairing the parts in the pump, the bearing needle rollers should be replaced. The requirements for needle rolling are: the dimensional error of all needle rolling diameters should not exceed 0.003mm, the allowable length deviation is 0.1mm, and the clearance with the shaft should be around 0.1mm; When assembling the rolling needles, they should be filled into the bearing housing according to the required quantity, and the rolling needles should be arranged parallel to each other.