
Current location: ENGLISh > NEWS > Company News >
Analysis of Oil Temperature and Fluid Problems in Hot Oil Pump
time:2025-07-16 10:58:25 author:特种泵阀 click:361
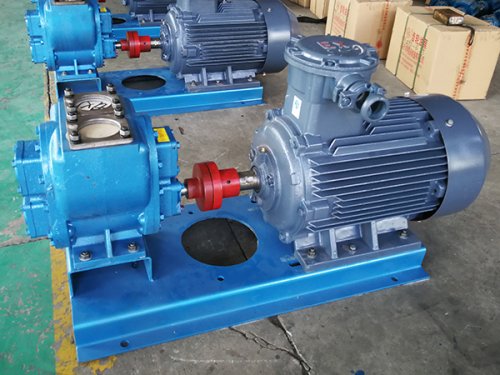
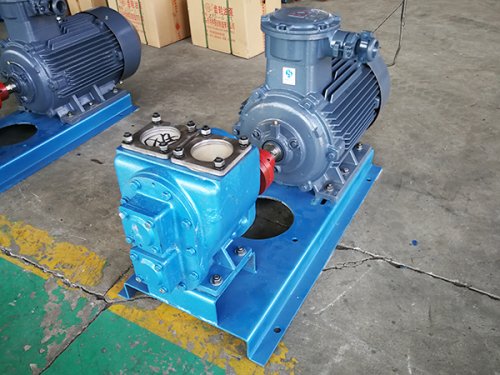
As the core equipment for transporting high-temperature media, the operational stability of the hot oil pump is closely related to oil temperature control and oil quality. In industries such as petrochemicals and asphalt processing, hot oil pumps are exposed to high temperatures of 200-400 ℃ for a long time. Abnormal oil temperature or deterioration of the oil will directly lead to an increase in equipment failure rate. This article systematically elaborates on the key issues and response strategies in the operation of hot oil pumps from four dimensions: oil temperature fluctuation mechanism, oil degradation characteristics, fault diagnosis, and preventive maintenance.
1、 Mechanism and Impact of Abnormal Oil Temperature Fluctuations
1. Causes of abnormal fluctuations in oil temperature
Heat source system failure: Fluctuations in temperature at the inlet and outlet of the thermal oil furnace (± 10 ℃ or above) will directly cause abnormal oil temperature in the pump body. It is necessary to check the flame stability of the burner, the flow rate of the circulating pump (should be ≥ 90% of the value), and the system pressure (normal fluctuation ≤ 0.05MPa).
Cooling system failure: For hot oil pumps with cooling jackets, insufficient cooling water flow (should be ≥ 5L/min) or high water temperature (>35 ℃) can cause the bearing oil temperature to exceed the limit. It is necessary to monitor the temperature difference between the inlet and outlet of the cooling water (normal value 8-12 ℃).
Internal leakage: When the mechanical seal leakage exceeds 5ml/h, high-temperature medium mixed with lubricating oil causes a sudden rise in oil temperature. A preliminary judgment can be made by observing the degree of oil emulsification inside the oil level mirror (>10% emulsion layer requires shutdown for maintenance).
2. Hazards of abnormal oil temperature
Sealing failure risk: When the oil temperature exceeds the temperature limit of the sealing material (fluororubber ≤ 200 ℃, graphite ≤ 400 ℃), the sealing element will harden and shrink, causing leakage. Actual test data shows that for every 10 ℃ increase in oil temperature, the sealing life is shortened by 30%.
Deterioration of lubrication performance: The viscosity of the base oil decreases exponentially with increasing temperature (the viscosity of ISOVG46 oil at 150 ℃ is only 1/5 of that at 40 ℃), resulting in insufficient lubrication of friction pairs such as gears and bearings.
The effect of oxidation acceleration: The Arrhenius equation shows that for every 10 ℃ increase in oil temperature, the oxidation rate accelerates by 2-3 times. For every 1mgKOH/g increase in oil acid value (TAN) at high temperatures, the lifespan of the oil is reduced by 50%.
2、 Characteristics and detection methods of oil degradation
1. Typical deterioration characteristics
Abnormal viscosity: Under normal operating conditions, the rate of change in oil viscosity should be ≤ ± 15%. If the measured viscosity is below the lower limit, fuel dilution may occur; If it exceeds the upper limit, there may be polymerization of oxidation products.
Excessive acid value: When the acid value is greater than 2mgKOH/g, the corrosiveness of the oil to metals is significantly enhanced. Regularly check the acid value of the oil and compare it with the initial value of the new oil (usually ≤ 0.5mgKOH/g).
Mechanical impurities: Laser particle size analyzer is used for detection. When the particle count (NAS1638 standard) exceeds level 8, centrifugal separation or replacement of the filter element (filtration accuracy should be ≤ 10 μ m) is required.
Moisture content exceeding the limit: When the Karl Fischer method detects a moisture content greater than 0.1%, it will cause oil emulsification and additive failure. Check the status of the desiccant in the respirator and the sealing of the system.
2. Testing techniques and methods
Infrared spectroscopy analysis: It can quickly detect characteristic functional groups such as oxidation products (carbonyl peak at 1710cm ⁻¹) and fuel dilution (CH ₂ stretching peak at 2920cm ⁻¹) in oil.
Iron spectrum analysis technology: By separating wear particles in oil through magnetic field, the wear status of different friction pairs such as bearings (spherical particles) and gears (strip-shaped particles) can be identified.
Dielectric constant monitoring: Online dielectric constant sensors can reflect the degree of oil contamination in real time (compared to clean oil, it should be taken seriously when the dielectric constant changes by more than 10%).
3、 Typical fault diagnosis and disposal
1. Mechanical seal leakage
Fault characteristics: Oil leakage in the bearing area of the pump body, abnormal increase in oil temperature, and infrared thermal imaging showing a temperature gradient of>30 ℃ in the sealing area.
Disposal measures: Check the wear of the sealing surface after shutdown (the width of the contact strip should be ≥ 2/3 of the sealing surface width), and replace the silicon carbide/tungsten carbide material pair (the hardness difference should be controlled within HRC2-3).
2. Bearing overheating failure
Fault characteristics: The vibration spectrum shows bearing fault characteristic frequencies (outer ring fault is BPFO, inner ring fault is BPFI), and the lubricating grease begins to carbonize when the temperature exceeds 100 ℃.
Disposal measures: After disassembly, check the bearing clearance (standard value 0.03-0.08mm), use a coordinate measuring instrument to detect the roundness of the raceway (≤ 0.005mm), and replace the high-temperature bearing (working temperature ≥ 200 ℃).
3. Oil emulsion
Fault characteristics: There is obvious oil-water stratification in the oil level mirror, with a sharp increase in acid value (>5mgKOH/g) and a decrease in viscosity of>30%.
Disposal measures: Immediately replace all oil, steam blow the system (temperature ≥ 150 ℃, pressure 0.3MPa), and replace the respirator desiccant (color changing silicone gel moisture absorption rate ≥ 30%).
4、 Preventive maintenance strategy
1. Intelligent control of oil temperature
Install PID temperature control system to control the oil temperature fluctuation range within ± 5 ℃. For high-temperature pumps (>300 ℃), it is recommended to use a dual circuit heating system (main circuit 350 ℃, backup circuit 320 ℃).
Install thermocouples in key parts of the pump body (bearing seat, gear chamber), establish a three-dimensional temperature field monitoring network, and automatically sound an alarm when the local hot spot temperature difference exceeds 20 ℃.
2. Oil quality management
Develop oil change cycle standards: mineral oil ≤ 2000h, synthetic oil ≤ 8000h. Use the Oil Health Index (OHI) for comprehensive evaluation, and change the oil in advance when OHI
Install an online oil monitoring system to collect real-time parameters such as viscosity, acid value, and moisture. When any indicator exceeds the threshold, a maintenance reminder will be triggered.
3. System optimization and renovation
Improved sealing structure: Adopting a series mechanical seal (pressure distribution ratio 1:2), the leakage rate can be reduced to below 0.1ml/h.
Optimize cooling system: For hot oil pumps, it is recommended to use a closed cycle cooling system (cooling water circulation utilization rate ≥), equipped with plate heat exchangers (heat exchange rate ≥ 90%).
The oil temperature and oil management of the hot oil pump need to be established; Monitoring Diagnosis Maintenance; Closed loop system. It is recommended to conduct a special inspection every quarter and establish a degradation trend model by comparing historical data. For critical equipment, digital twin technology can be introduced to predict oil life and equipment status through virtual simulation. By implementing full lifecycle management, the mean time between failures (MTBF) of hot oil pumps can be increased to over 12000 hours, and maintenance costs can be reduced by over 40%.